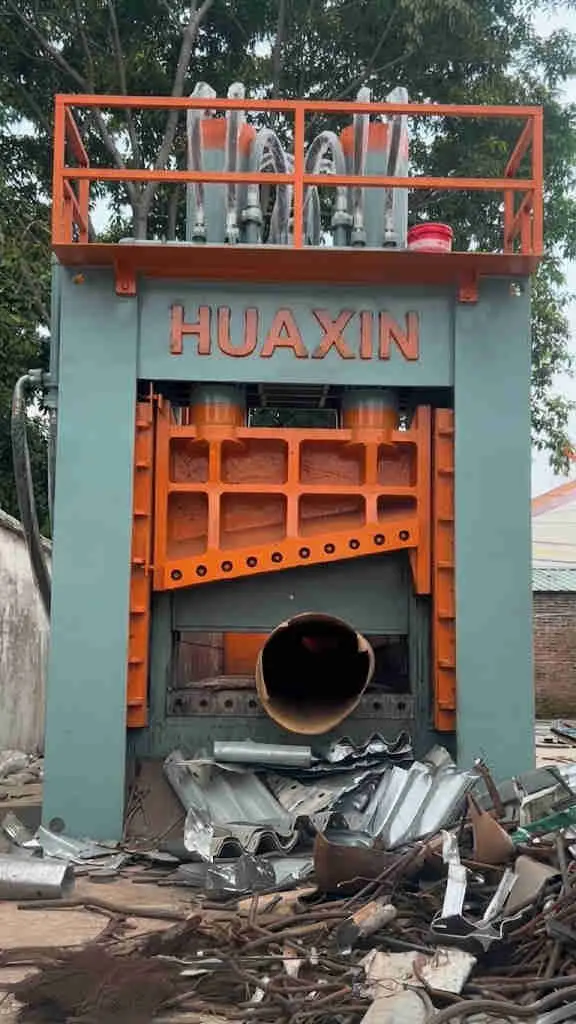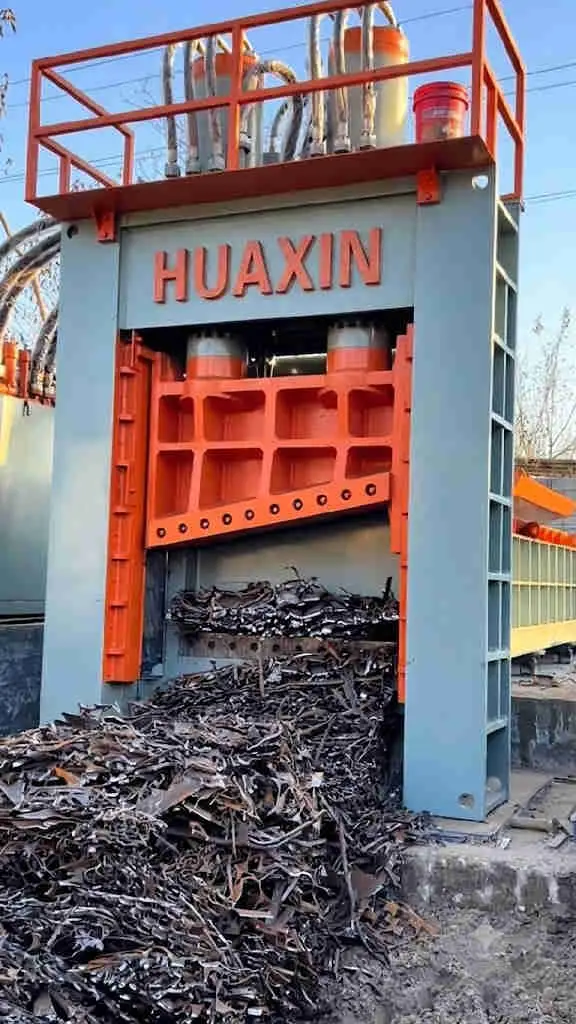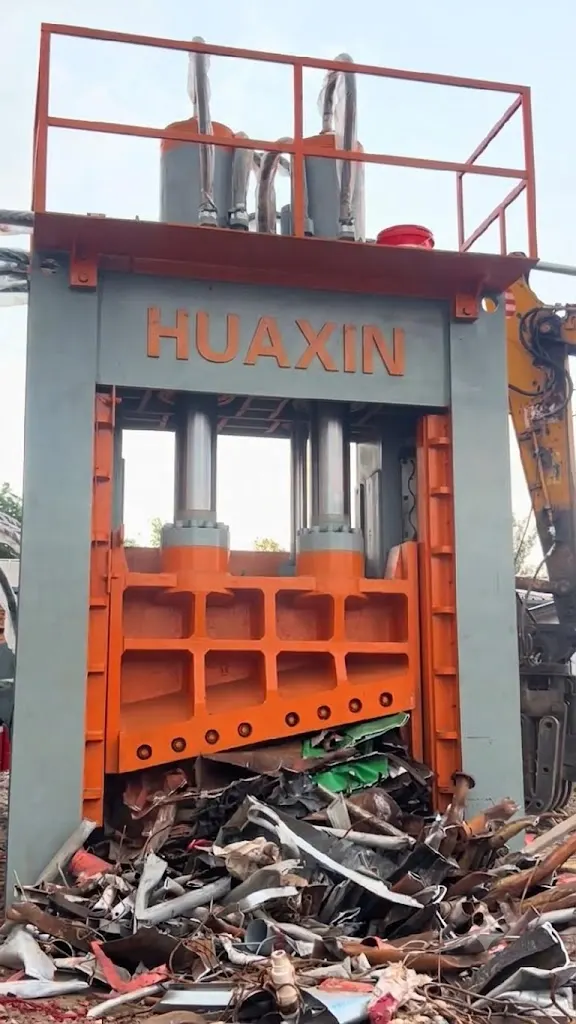
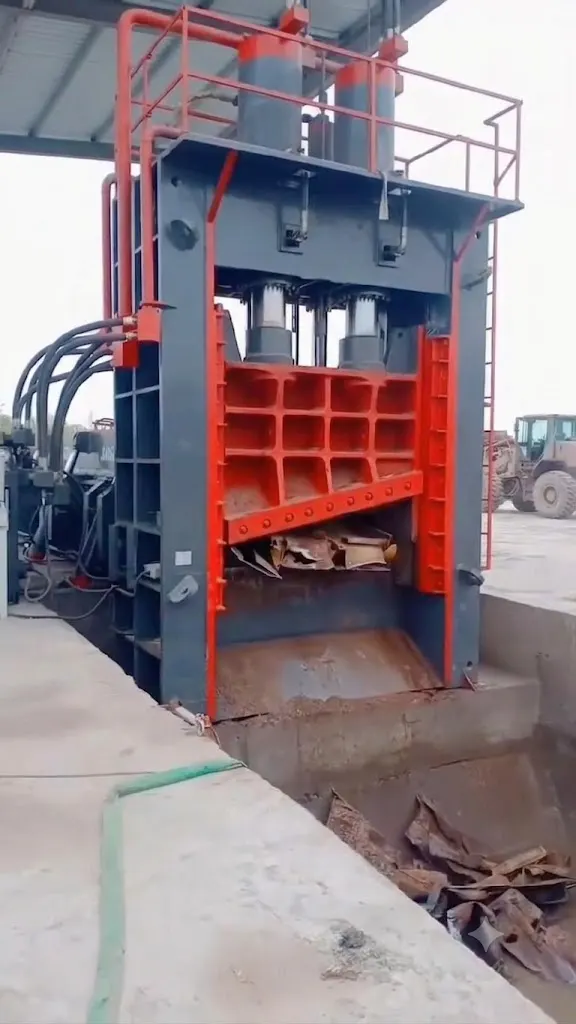
Shipbreaking is the heaviest, dirtiest cutting a shear is asked to do. Hull plate is thick and continuous, the structure behind it is heavy and irregular, and the feed arrives with marine growth, paint and non-steel attached. A 1000 ton gantry shear is where shipbreaking becomes a production question rather than a struggle. It brings 1,000 t of force, mild steel plate up to 100 mm as continuous duty, and 100 to 120 tons a day. This article covers what the material demands. Across our industrial scrap metal shear installations, material preparation and hydraulic maintenance decide long-term profitability more than any single specification line.
Why ship plate is a class above
Hull plate is thick, and thickness is only the start. The plate arrives in large, irregular pieces cut from a structure that was never designed to be taken apart. Stiffeners, brackets and doubler plates are often still attached. Each attachment hits the blade before the plate does, and the irregular shape means the piece rarely lies flat in the box. That combination is what pushes shipbreaking toward the production classes.
The 1000-ton class carries ship plate as continuous duty up to its 100 mm rating, and the force rule covers the headroom check. On shipbreaking the check matters more than anywhere else. The material arrives close to the limit of what a yard machine can take, and heavy pieces come every week rather than every month.
For hull work that needs more than 1000 tons, the 1250, 1600 and 2000-ton classes are in our scrap metal gantry shear range.
What the duty rating means for a 1000 ton gantry shear at ship scale
Shipbreaking is continuous duty in the literal sense. The feed never stops, the material is always heavy, and the machine runs shift after shift on the hardest thing it was built to take. The duty declaration separates a shipbreaking machine from a yard machine of the same force class. Frame, hydraulics, cooling and wear specification are all quoted against the declared shift pattern, and a shipbreaking yard often declares three shifts.
The difference shows up in year three. A machine quoted for the duty holds its published figures through the season. A machine quoted for a lighter pattern fights the operation, and the fight appears as stretched cycles beyond the 20–35 second band and shorter blade intervals, not as a fault anyone can point at. Our three-shift economics guide prices the hours and covers what a third shift adds.
Spares depth at ship scale
At shipbreaking volume a wear part is a logistics question before it is a maintenance one. The shelf set exists so a rotation never waits on a shipment: one blade set, the seal kit and the filter stock, sized to the season rather than to a standard kit. Resupply covers the rest, and the commissioning plan has the crew perform each replacement procedure rather than watch a demonstration.
The reason is arithmetic. A shipbreaking yard loses a shift’s output when a blade set is down. A procedure the crew has performed once is a planned change. A procedure they have only read about is a stop. The 1000-ton product page lists the four-edge reversible blades in H13, M6V, X45 or D2 tool steel that the shelf set is built around.
The feed discipline shipbreaking demands
Shipbreaking feed is dirty, and the dirt is the wear budget. Marine growth, paint and attachments all hit the blade before the steel does. A sorting gate at intake keeps blade life predictable. One pass strips the attachments and sets aside the non-steel, and the machine cuts steel instead of whatever the crane brought.
The HMS 1 and 2 guide covers the same charging logic on other heavy feed, and the blade maintenance guide covers the rotation discipline that keeps the interval visible. On shipbreaking the gate is the first line of the blade budget.
What the structure behind the plate adds
Hull plate rarely arrives alone. Behind it are frames, longitudinals, brackets and stiffeners, and each one changes the cut. A stiffener running across the cut line loads the blade unevenly. A bracket at the edge of a piece catches the blade corner and chips it. A piece that is mostly plate with a heavy frame attached behaves like two materials in one.
The sorting gate separates what it can, but on ship structure the geometry matters more. The piece has to lie in the box so the cut line is presented clean. The feeding guide covers orientation habits. The blade guide covers the 1,800 or 2,000 mm blade choice that takes a whole frame member without repositioning.
The discharge plan at shipbreaking volume
Shipbreaking output is heavy in a way that overwhelms a yard’s normal handling. Cut plate and section leave the box as dense, awkward pieces, and the discharge has to take them at the box’s rate. A destination sized for light scrap banks up under hull plate. Then the machine waits with a full box while handling catches up.
Size the buffer and destination for the heaviest routine piece, not the average, and test the plan against a week of late trucks. The 20 tons per hour guide covers the flow arithmetic. On shipbreaking the discharge is usually where the 10–12 t/h band is won or lost, because the machine can cut faster than handling can clear.
Why the blade log matters most here
Shipbreaking wears blades faster than any yard feed, and a log keeps the wear visible. Record three lines per rotation: date, tonnage since the last one, dominant material. Three months of entries show the interval your ship plate actually needs. They also catch silent changes, such as a new supplier or a heavier hull section, before they reach the blade bill.
The yard that keeps the log adjusts the interval to the material. The yard that skips it finds the change at the worst moment, which at ship scale is mid-season. The maintenance guide covers the mechanics. The log is the one habit that separates a shipbreaking machine that holds its rate from one that fights it.
What the heaviest routine piece is, measured
The class conversation on shipbreaking always comes back to one measurement: the heaviest routine plate, with its attachments, as it actually arrives. Ignore the record piece from the largest vessel, and ignore the average. Measure the plate that arrives weekly with a tape, and weigh it if you can. That number settles the class, and most buyers never take it.
It matters because the machine’s limit is set by the weekly piece. A yard that sizes for the record piece buys force it uses once a month and pays for it every other day. A yard that sizes for the average runs at its limit on the weekly heavy piece and wears blades for it. If weekly plate runs past 100 mm, look at the 1250-ton class, rated for 120 mm continuous. The measurement takes an afternoon.
Shipbreaking FAQ: 1000 Ton Shear
What ship plate can a 1000 ton shear cut?
Mild steel hull plate up to 100 mm as continuous duty. Attachments and irregular shapes are part of the material, and the sorting gate strips what the blade should not see.
Is shipbreaking a different build from a yard shear?
Same force class, different duty declaration. A shipbreaking machine is quoted for continuous multi-shift duty on the hardest feed, and its frame, cooling and wear specification follow that declaration. Every machine is load-tested at the factory before shipment.
How much spares depth does shipbreaking need?
A shelf set sized to the season: one blade set, the seal kit and the filter stock, in place before commissioning. Resupply covers the rest, and the crew performs each procedure before the season starts.
What do you need to quote a shipbreaking machine?
The plate thickness range, the shift pattern, the season length, and the discharge and handling plan. You will have a written quotation within 48 hours, with the duty declaration restated as the build basis.
Sizing cutting force, blade length and hydraulic power for ship plate? Compare full machine parameters on our 1000 Ton Scrap Metal Shear page, review our gantry and NS scrap shear hub, or contact HUAXIN’s Tangshan engineering team with feedstock photos and your target daily tonnage.