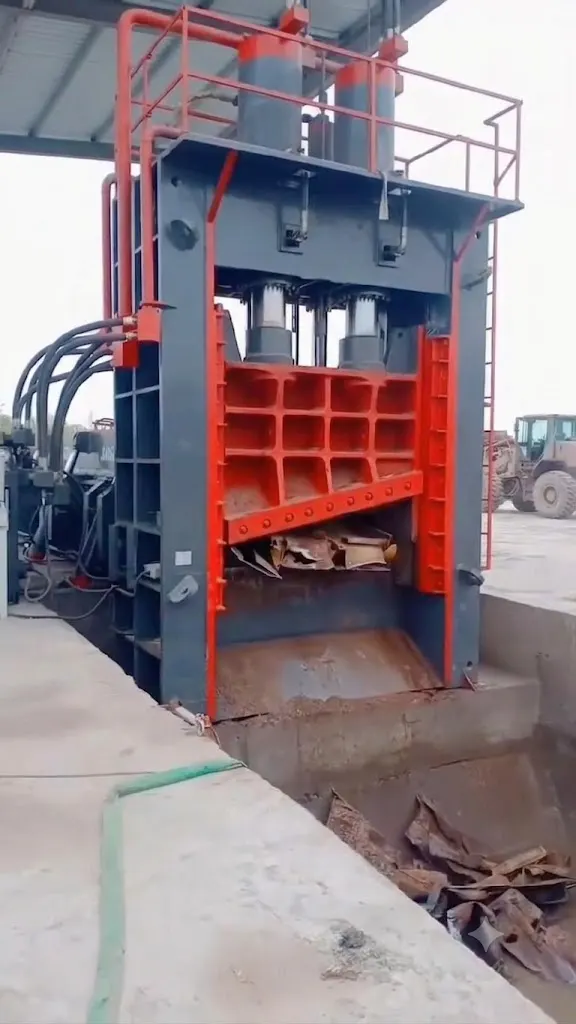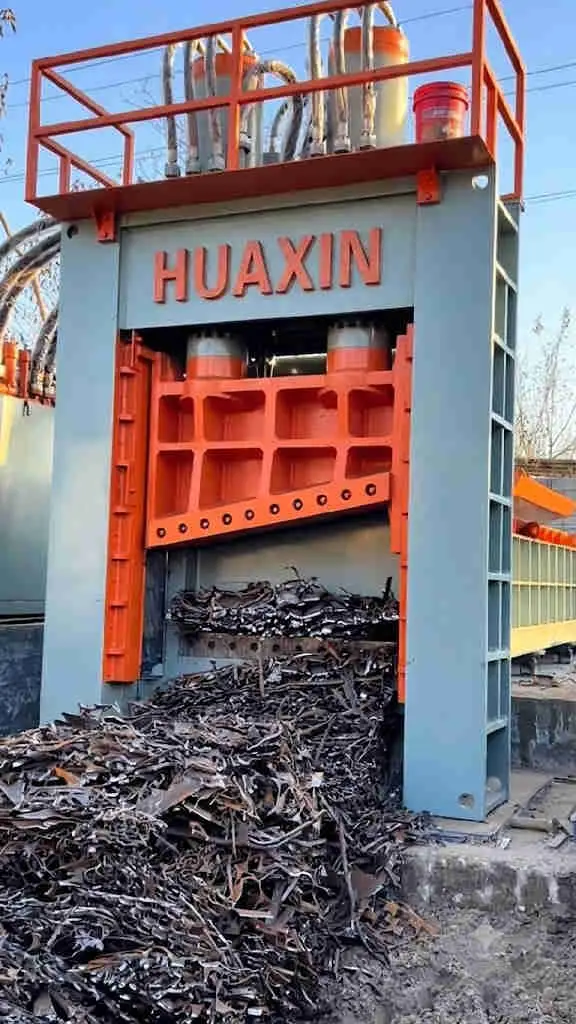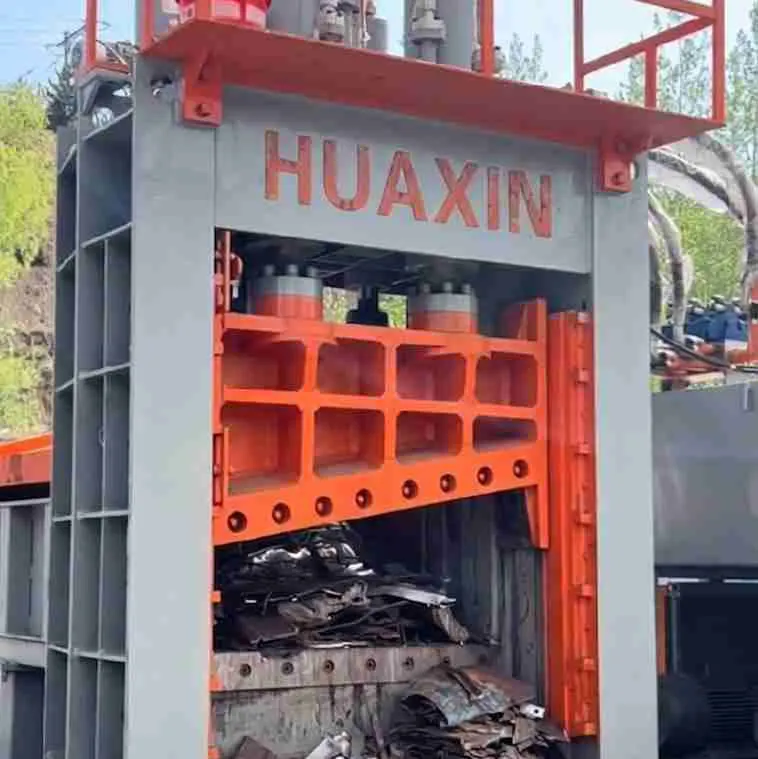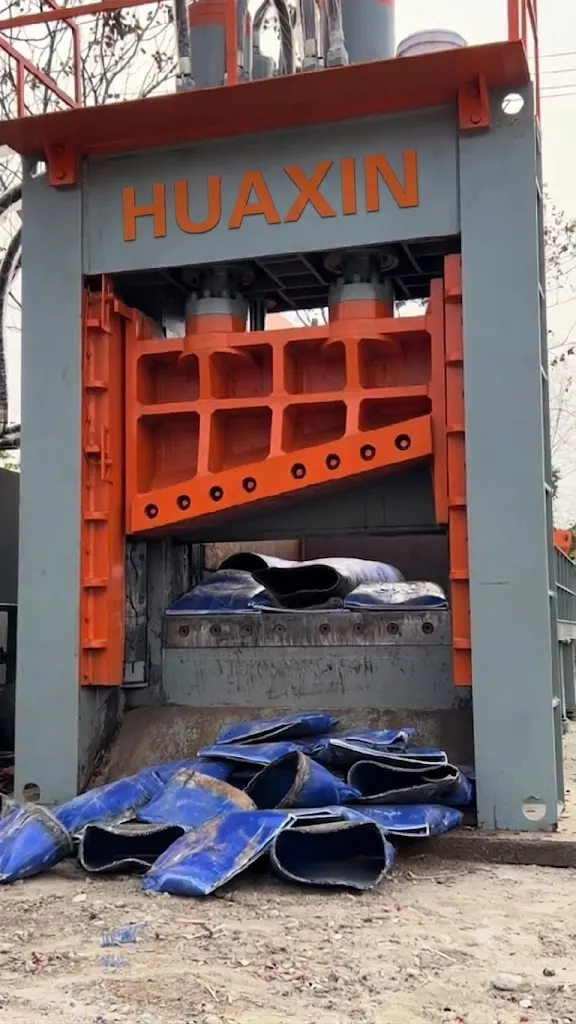
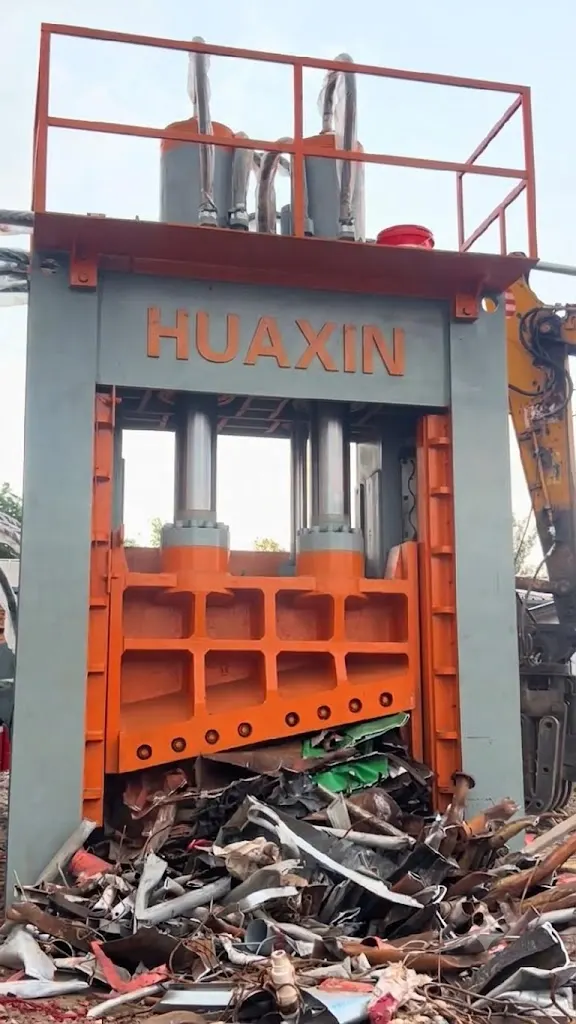
Structural steel is where a gantry shear earns its keep, and beams are the material that tests it. An I-beam is not a thick plate or a bundle of bar; it is a section with flanges and a web, and how it cuts depends on how it enters the box. The 400 Ton Scrap Metal Shear Machine (Q91-400) is the class most structural yards land on, and this article covers what cutting beams cleanly actually requires. If you are comparing gantry and alligator shear configurations, production runs on the 400 Ton Scrap Metal Shear (Q91-400) illustrate how cutting force and operator discipline impact hourly output.
Why beams are a different cut
A beam cuts differently from plate because it is not solid. The flanges carry the load at the edges, the web carries it in the middle, and a clean cut happens when the blade works through all three without the section twisting. When a beam twists under the blade, the cut strays, the edge wears on one corner, and the cycle stretches. The difference between a clean beam cut and a messy one is mostly feed orientation and hold-down, which is why the class and the configuration are two separate decisions.
The 400 sits at the natural entry point for structural work. Its published material table covers light to medium sections, and beams that arrive as demolition or fabrication offcuts sit comfortably inside that range. The Q91-400 page carries the specification rows worth checking against the beam you actually receive.
What section depth does to the force
Section depth is the number that matters more than the beam’s weight. A deep section puts the flanges further from the web, and the blade has to work through more unsupported metal between them. The force class follows the deepest routine section, not the heaviest single piece, because depth is what makes a beam want to twist. A shallow beam cuts clean on a smaller machine; the same tonnage in a deep section wants the class above.
The practical check is to measure the deepest beam that arrives weekly and compare it against the machine’s published section range. The force rule covers the headroom logic, and it is arithmetic rather than judgment. Where the depth sits inside the range, the 400 cuts clean; where it pushes past, the conversation moves up.
Orientation decides the edge
A beam laid flat cuts differently from a beam fed on edge. Laid flat, the flanges hit the blade first and the web follows, and the cut is stable. Fed on edge, the beam presents a taller, thinner section that twists more easily under load. The right orientation depends on the section, and the crew learns it in the first week or it never sticks.
The hold-down is the other half. A beam that is clamped before the stroke cuts clean; a beam that shifts mid-cut wears one corner of the edge and strays off square. The feeding discipline guide covers the habits, and the maintenance guide covers what a twisted cut does to the blade interval.
When the beam is too long for the box
The force class is only half the fit. A beam that is too long for the box has to be repositioned, and every reposition is a minute the machine is not cutting. The blade length and the box opening decide the length the machine takes whole, and the beam that forces a reposition is the most common throughput loss on structural feed.
Count the over-length beams in a normal week and multiply by the minutes each reposition takes. The annual figure is the cost of a too-short configuration, and it usually dwarfs the price difference between blade options. The box guide covers the geometry, and the blade guide covers the length side.
What the blade does to a beam it does not like
A beam that pushes past the machine’s range does not get refused. It gets cut badly, and the bad cut shows up in three places. The edge chips on one corner, where the unsupported flange loaded it first. The cycle stretches, because the machine works harder for the same cut. And the rotation interval shortens, which is where the wear bill arrives. None of it is a dramatic failure, and all of it shows up in the blade log before it shows up anywhere else.
The blade steel guide covers what the specification should say about grade and hardness for structural feed, and the cycle guide covers what a stretching cycle is telling you from the control station.
Why the sorting gate earns its keep on beams
Structural steel rarely arrives clean. Beams come with bolts, brackets, gusset plates and the occasional non-steel still attached, and each of those hits the blade before the steel does. The sorting gate is the position at intake that separates the clean beam from the beam with attachments, and on structural feed it is the cheapest wear insurance in the yard.
The gate is not housekeeping; it is the wear budget’s first line. A yard that runs it gets blade intervals close to the published figures. A yard that feeds whatever the crane brings gets shorter intervals on the same machine and the same beams, and the difference shows up in the rotation log within a month. The charging discipline guide covers the same logic on heavier material.
Reading the specification rows for structural work
A structural yard should read three rows on the specification more carefully than the rest. The chamber dimensions, because they set the widest beam the machine admits. The blade length options, because they set the longest beam it cuts in one pass. And the hold-down specification, because it is what keeps a beam from twisting mid-cut. Together the three rows are the geometry, and the force rating sits on top of them.
The sheet reading guide covers how the rows relate, and the gaps guide covers the six things no sheet carries, including the duty basis the rating assumes. Reading all three rows against your own beam measurements is the difference between a machine that fits and one that fights.
What changes when the beams arrive in a teardown
Demolition beams are a different feed than fabrication offcuts, even at the same section size. Teardown steel arrives dirty, with concrete, bolts and non-steel still attached, and it arrives in pieces that were never cut to length. The same 400 class cuts both, but the feed discipline differs: teardown feed wants the sorting gate running full time, and the geometry wants the widest beam from the demolition rather than the widest from the shop.
If teardown is a growing share of the intake, the geometry conversation moves, and the step-up guide covers where the structural classes sit relative to the demolition feed. The machine is the same; what changes is what you measure before you buy.
Engineering & Field FAQ: Cutting I-Beams and H-Beams Cleanly on a 400 Ton Shear
What beams can a 400 ton shear cut?
Light to medium I-beams and H-beams, the kind that arrive as demolition or fabrication offcuts, within the published section range. The deepest routine beam is the measurement that decides, not the heaviest single piece.
Why does section depth matter more than weight?
Because a deep section twists more easily under the blade, and twisting is what strays the cut and wears one corner of the edge. Two beams of the same weight can need different classes if one is a shallow heavy section and the other is deep.
How do I check the fit against my beams?
Measure the deepest beam that arrives weekly and compare it against the published section range. If it sits inside, the class is right. If it pushes past, the conversation moves up. The measurement takes an afternoon with a tape measure.
What do you need to recommend the right class?
The deepest routine beam, how often beams arrive, and your daily tonnage. The written recommendation comes back within two business days, including when the answer is the class below the one you asked about.
What is the biggest mistake structural buyers make?
Sizing for the tonnage instead of the section. Two yards can move the same daily tonnage and need different classes if one receives deep beams and the other receives shallow sections, because depth is what makes a beam want to twist under the blade. The deepest routine beam is the measurement that settles it.
Summary Checklist: Cutting I-Beams and H-Beams Cleanly on a 400 Ton Shear
Beams are the material a gantry shear earns its keep on, and the 400 class is the natural entry for structural work. The fit is three measurements: the deepest beam, the widest beam, and the longest beam, checked against the published rows before the order. Get the force, the box and the blade all matched to the beam you actually receive, and the machine disappears into the production plan. Get any one of them wrong, and the beam wins every shift. Send the three measurements, and the recommendation comes back in writing within two business days, built around the beam you actually receive rather than the one you hope to.
Evaluating equipment specifications or FOB/CIF delivery schedules for your plant? Compare full machine parameters on our 400 Ton Scrap Metal Shear (Q91-400) page, review our scrap metal shear engineering hub engineering hub, or contact HUAXIN’s Tangshan engineering team with your feedstock photos and target daily tonnage.